What Is Industrial Activated Carbon?
Industrial activated carbon is an indispensable material for modern industry and plays a key role in many fields. This unique adsorbent has become a central component of purification, separation and recovery processes due to its excellent properties. In this article, we will take an in-depth look at the definition, production process, properties and wide range of applications of industrial activated carbon.
Industrial Activated Carbon Definition and Basics
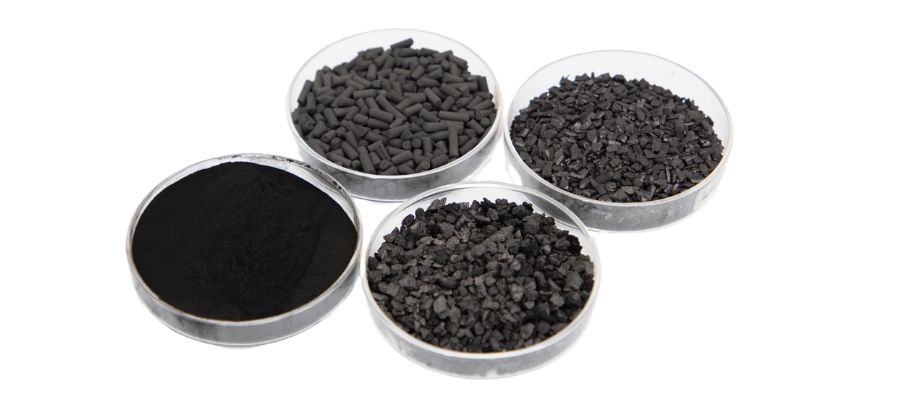
Industrial activated carbon is a highly porous carbon material with a large specific surface area and powerful adsorption capacity. It is produced by activation treatment of various carbonaceous materials, a process that creates a complex internal pore structure that can adsorb a wide range of contaminants in gases and liquids.
The key feature of industrial activated carbon is its developed pore structure, which includes micropores (<2 nm), mesopores (2-50 nm), and macropores (>50 nm). This diversified pore distribution allows it to adsorb molecules of different sizes and types, making it suitable for a variety of industrial applications.
Compared to domestic or commercial activated carbon, industrial activated carbon generally has a higher purity, larger specific surface area and stricter quality control standards to meet complex industrial demands.
Industrial Activated Carbon Production Process
The production of industrial activated carbon involves several key steps:
- Raw Material Selection: Common raw materials include coconut shells, charcoal, wood, etc. Each raw material imparts unique characteristics to the final product.
- Carbonization: The feedstock is heated to 400-900°C in an oxygen-free environment to remove volatile substances and form the initial carbon structure.
- Activation: Physical activation is oxidation at temperatures of 800-1000°C using water vapor, carbon dioxide or air. Chemical activation is carried out at lower temperatures using chemical reagents such as phosphoric acid and zinc chloride.
- Cooling and washing: The activated product is cooled and washed to remove residues.
- Sifting and grading: Activated carbon is classified into different sizes and shapes according to different application requirements.
- Quality control: Rigorous testing is performed to ensure that the product meets industry standards.
At PuroCarbon S.L., with more than 18 years of experience in the production of activated carbon, we can offer a variety of high quality industrial activated carbons, including Coconut Shell Activated carbon, Coal-Based Activated Carbon and activated wood charcoal, among others.
Characteristics and Properties of Industrial Activated Carbon
Industrial activated carbon possesses several key characteristics that make it excel in industrial applications:
- High specific surface area: Generally between 500-2500 m²/g, providing a large number of adsorption sites.
- Diversified pore structure: Suitable for the adsorption of molecules of different sizes.
- Chemical stability: Maintains stability in most environments, suitable for various applications.
- Thermal stability: Capable of maintaining performance in high temperature conditions.
- Regenerability: Many types of industrial activated carbon can be regenerated and reused by thermal or chemical methods.
- High adsorption capacity: Can effectively remove various contaminants, including organic compounds, heavy metals, etc.
- Selective adsorption: Some specially treated activated carbons can perform selective adsorption of specific pollutants.
- Mechanical resistance: Especially granular and pelletized activated carbons have good mechanical resistance, suitable for continuous flow systems.
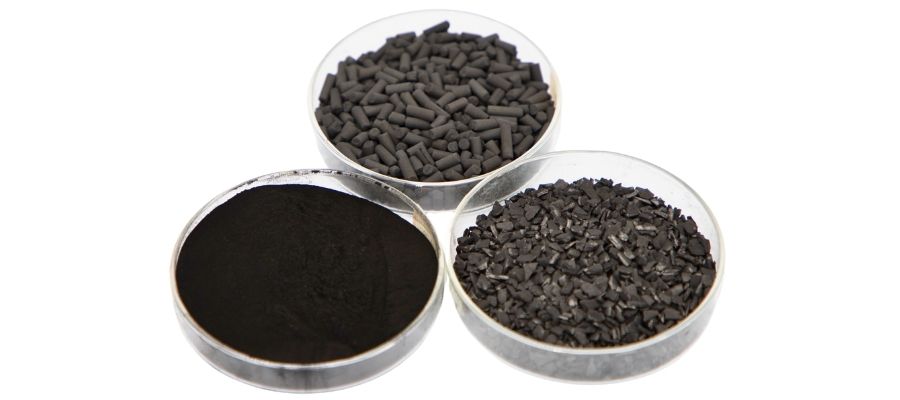
These characteristics make industrial activated carbon an ideal choice for purification and separation processes. At PuroCarbon S.L., we offer activated carbon in various forms, including Activated carbon pellets, Powdered activated carbon and Granular activated carbon, to meet the needs of different industrial applications.
Industrial Activated Carbon Application Areas
Industrial activated carbon plays an important role in numerous fields:
water treatment

- Municipal water treatment: Removal of organic contaminants, chlorine, odors, etc. from water.
- Industrial wastewater treatment: Removal of heavy metals, organic solvents and other pollutants.
- Groundwater remediation: Adsorption of contaminants in soil and groundwater.
Air purification

- Industrial waste gas treatment: removal of volatile organic compounds (VOCs), sulfur compounds, etc.
- Indoor air purification: Elimination of harmful gases such as formaldehyde, benzene, etc.
Food and Beverage Industry

- Decolorization: Used for decolorization of syrups, vegetable oils, etc.
- Odor elimination: Elimination of unwanted tastes and odors.
Pharmaceutical Industry
- Purification of medicines: Removal of impurities and colors.
- Medical equipment: Used in gas masks, dialysis equipment, etc.
Chemical Industry
- Catalyst support: As a carrier for various catalytic reactions.
- Solvent recovery: Adsorption and recovery of organic solvents.
Metal extraction

- Gold recovery: Adsorption of dissolved gold in the gold extraction process.
Environmental Remediation
- Soil remediation: Adsorption of organic contaminants in soil.
- Oil spill treatment: Adsorption of oil on the water surface.
Automotive industry
- Vapor canisters: Control of fuel evaporation in automobiles.
Electronics industry
- Supercapacitors: As electrode material.
At PuroCarbon S.L., we offer customized solutions for these diverse applications, including specially treated products such as acid-washed activated carbon and Impregnated activated carbon to meet specific industrial needs.
Considerations for the Selection and Use of Industrial Activated Carbon
The selection of the right industrial activated carbon requires consideration of multiple factors:
- Type of application: Different applications may require different types of activated carbon.
- Nature of contaminant: Organic, inorganic, gaseous or liquid contaminants may require specific activated carbons.
- Treatment conditions: Operating conditions such as temperature, pH, flow rate, etc., will influence the selection.
- Required adsorption capacity: Select the appropriate amount of activated carbon according to the concentration of the pollutant and the volume to be treated.
- Regeneration needs: If multiple use is required, a type of regenerable activated carbon should be selected.
- Economic factors: Consider initial cost, operating costs and possible regeneration costs.
- Environmental impact: Choose sustainable and environmentally friendly types of activated carbon.
Correct selection and use can significantly improve the efficiency and economy of the industrial process.
Conclusion
Industrial activated carbon is an indispensable multifunctional material in modern industry, whose unique adsorption properties play a key role in numerous fields. From water treatment to air purification, from chemical separation to environmental remediation, industrial activated carbon has become the ideal choice for solving complex industrial challenges thanks to its efficient, diverse and sustainable characteristics.
If you are looking for efficient and reliable industrial activated carbon products, or need professional technical support, please do not hesitate to contact us. contact us atLet's work together to explore the endless possibilities of industrial activated carbon and bring new vitality to your business!